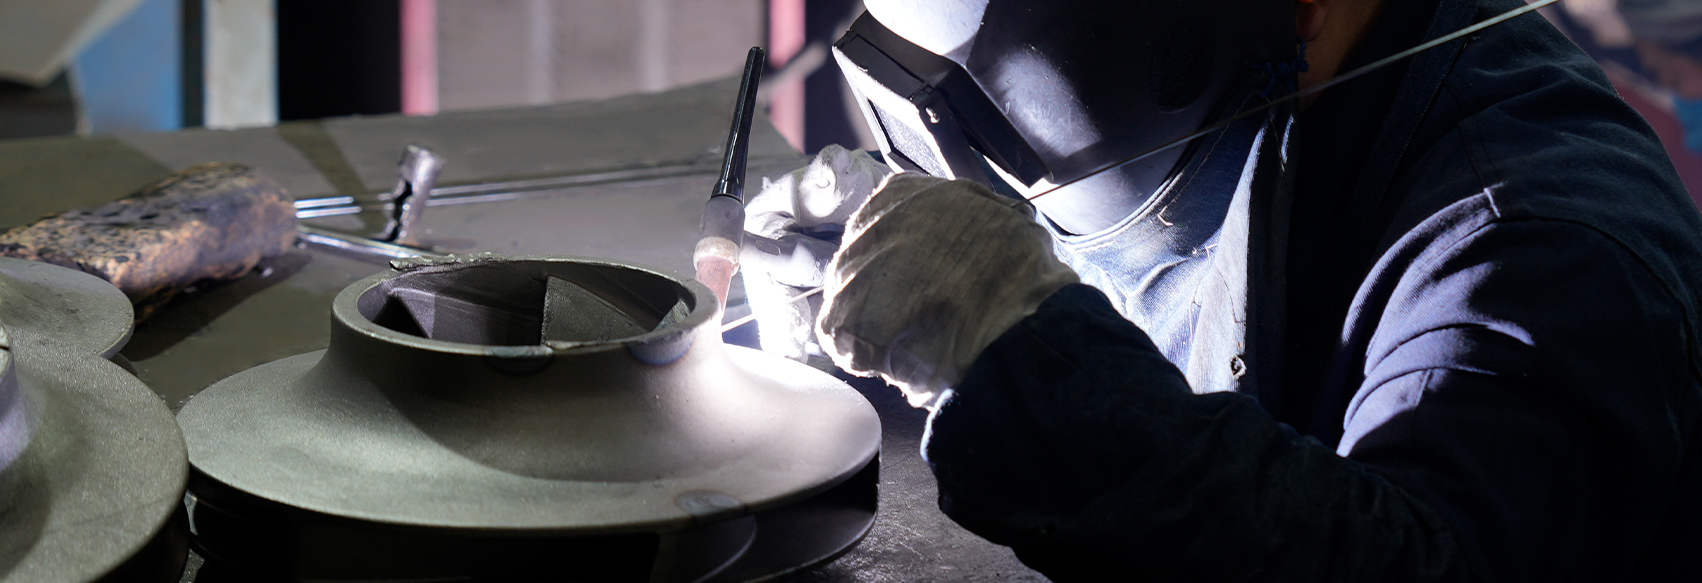
A replacement order for a pump sleeve usually begins with a question: the previous part failed by pitting near the flange after eighteen months, and the plant engineer wants a casting that will last until the next major turnaround. Corrosion-resistant castings are rarely judged by tensile strength alone. In chemical, heat treatment, and steel processing plants, the deciding factors are alloy composition, casting process, heat treatment, and internal soundness. This article explains how those factors work together, how to compare grades, and what to verify before a casting goes into service.
What Is a Corrosion-Resistant Casting?
A corrosion-resistant casting is a metal component shaped by pouring molten alloy into a mold, then engineered to resist the chemical attack expected in its service environment: pitting, crevice corrosion, stress corrosion cracking, or high-temperature oxidation. The material families most often used in industrial castings are:
- Austenitic stainless steels such as 316L (CF3M casting grade), with good all-round resistance to many acids and chloride-bearing media at moderate temperatures.
- Duplex stainless steels such as 2205 (CD3MN casting grade), combining higher strength with better resistance to chloride stress corrosion cracking than ordinary austenitic grades.
- Nickel-chromium alloys such as HP-type 26Cr35Ni, chosen when the component faces both high temperature and corrosive process atmospheres.
A casting is not a wrought part with a different shape. During solidification, cast alloys develop a coarser grain structure, can segregate at the dendrite level, and may contain microshrinkage when the feeding system is poor. All three features influence corrosion resistance. Two castings with the same nominal grade can therefore perform very differently depending on the foundry that produced them.
Corrosion Mechanisms That Determine Grade Choice
Before choosing a grade, identify which failure mechanism is most likely. Four dominate in industrial corrosion-resistant castings:
- Pitting and crevice corrosion: localized attack, usually driven by chlorides, and accelerated in stagnant areas, under gaskets, or beneath deposits.
- Stress corrosion cracking: tensile stress combined with a specific environment, such as hot chlorides or caustic solutions; it often produces sudden, unexpected fracture.
- Intergranular corrosion: attack along grain boundaries, typically caused by chromium carbide precipitation when the alloy becomes sensitized during casting, welding, or slow cooling.
- Uniform corrosion: even thickness loss across the surface; simpler to predict, but it still dictates the required wall thickness and service life.
The table below connects these mechanisms to the usual alloy response.
Common corrosion mechanisms and the typical alloy response used to counter them.
| Mechanism |
Typical environment |
Alloy direction |
| Pitting and crevice corrosion |
Chloride-rich liquids, seawater, oxidizing chloride bleach |
Higher chromium, molybdenum, and nitrogen; duplex grades such as 2205 (CD3MN) outperform 316L in most chloride services |
| Stress corrosion cracking |
Hot chlorides, caustic solutions, sour gas |
Duplex stainless or high-nickel austenitic grades; also reduce surface tensile stress |
| Intergranular corrosion |
Welded or sensitized sections exposed to acids |
Low-carbon grades such as CF3M, or solution annealing after welding |
| Uniform corrosion |
Strong acids, low-pH streams |
Higher total alloy content; nickel-base alloys in severe cases |
Alloy Selection: Start with PREN, Then Look Deeper
The Pitting Resistance Equivalent Number (PREN) is a standard screening tool for chloride pitting resistance: PREN = %Cr + 3.3 x %Mo + 16 x %N. It ranks austenitic and duplex grades quickly. The bars below show approximate values for common casting grades.
316L (CF3M) - PREN ~26
317L (CG3M) - PREN ~30
2205 (CD3MN) - PREN ~35
25Cr super duplex - PREN ~42
PREN is a starting point, not a final answer. It says nothing about uniform corrosion in reducing acids, and it cannot detect casting defects that act as pitting initiation sites. For critical components, pair PREN with corrosion test data or service experience. A 2205 duplex casting will usually survive hot chloride service that quickly pits 316L, but only if the microstructure is correct after solution annealing. When the heat treatment is wrong, harmful phases form at grain boundaries and the casting becomes vulnerable even though its chemistry meets the certificate.
How the Casting Process Changes Corrosion Performance
The casting route directly affects corrosion behavior because it determines grain structure, porosity, and surface quality. Three processes dominate corrosion-resistant component production, and each leaves a different signature.
- Centrifugal casting is preferred for cylindrical components: corrosion-resistant sleeves, radiant tubes, furnace rolls, and pipe sections. The metal solidifies directionally from the outer wall inward, producing a dense, fine-grained structure with few shrinkage voids. Centrifugal casting can produce parts from 50 mm to 1000 mm in diameter and up to 4000 mm in length.
- Investment casting (lost wax) is chosen for complex geometries, thin walls, and good as-cast surface finish. Because the shell mold stays warm, the metal can cool slowly unless pouring and mold temperature are controlled, so solution annealing after casting is critical.
- Resin sand molding suits large parts such as pump casings, valve bodies, and stirrers. Heavy sections cool unevenly, increasing the risk of segregation and carbide precipitation. These parts depend even more strongly on a correctly designed heat treatment cycle.
The practical conclusion is to state the required heat treatment together with the grade, including annealing temperature and cooling method and, where relevant, the permitted range for hardness and ferrite content.
What to Check When You Buy Corrosion-Resistant Castings
Procurement problems usually come from incomplete specifications rather than poor luck. A robust specification for a corrosion-resistant casting should include:
- A casting grade with a chemical composition range from casting standards such as ASTM A743, ASTM A744, or ASTM A890, rather than a wrought plate or bar standard.
- A heat-treatment requirement, usually solution annealing, expressed with a temperature range and a cooling method, plus acceptance limits for hardness and, for duplex grades, ferrite content.
- Non-destructive testing requirements: liquid penetrant testing for surface cracks, radiography for internal soundness, and hydrostatic testing for pressure-containing parts.
- Documentation: a material test certificate with the actual ladle analysis, plus spectrometer and metallographic reports for critical castings.
- Dimensional tolerances and any machining requirements tied to the drawing.
A foundry's verification hardware matters here. Direct-reading spectrometers confirm the actual chemistry of each heat, metallographic analysis verifies the structure after heat treatment, and 3D scanning checks that the delivered geometry matches the model. A casting with an excellent nominal composition can still fail early if it carries embedded defects.
Where Corrosion-Resistant Castings Are Used
Corrosion-resistant castings are rarely a commodity purchase; they are specified for duty. Typical applications include:
- Chemical and petrochemical plants: 2205 and 316L corrosion-resistant sleeves for process piping, HP-type 26Cr35Ni stirrers for reactors, and valve or pump components in aggressive media.
- Heat treatment and steel processing: radiant tubes, furnace rolls, and furnace bottom rolls that face high temperature combined with oxidizing, sometimes sulfidizing, atmospheres.
- Waste incineration: grate components and heat exchanger elements exposed to combustion gases and chloride-rich deposits.
The economic stake is larger than the part price. Industry studies estimate the global cost of corrosion at roughly $2.5 trillion, about 3.4% of global GDP, and most of that cost appears as lost production and unscheduled shutdowns, damage that often starts with a locally corroded casting.
Corrosion-resistant castings reward a disciplined approach. Identify the corrosion mechanism, verify the grade and heat treatment, and confirm internal soundness before the part reaches the line. A manufacturer such as Wuxi Dongmingguan Special Metal Manufacturing that controls melting, centrifugal and investment casting, heat treatment, machining, and quality inspection under one roof can answer these questions with its own data. When you evaluate a supplier, ask three questions: how was the part solidified, how was it heat-treated, and how do you know the delivered chemistry matches the certificate? The answers separate castings that merely carry a grade name, such as 316L or 2205, from castings that actually last in service.


 English
 Español
 عربى